
MECHANICAL SEALS FOR THE MINING INDUSTRY
Mining and minerals

OVERVIEW
Which technology is the best fit for your mining application?
Mines are complex operations that use large volumes of water and harsh chemicals across a wide range of processes.
Pumps are used to move liquids through the production process and drain underground water. Compressors transport gases and air, conveyors move crushed ore and autoclaves, and agitators support the processing and breakdown of minerals. Across all these different applications, reliable mining equipment seals play a critical role in maintaining operational efficiency.
Choosing the right mining sealing, packing, couplings, filtration or bearing isolator technology is essential for maximising the performance and reliability of each type of equipment.
John Crane offers a broad portfolio of solutions for the mining industry, designed to support pumps, compressors and other rotating equipment used in a mine.
Explore John Crane’s solutions for the mining and minerals industry

Type 5860
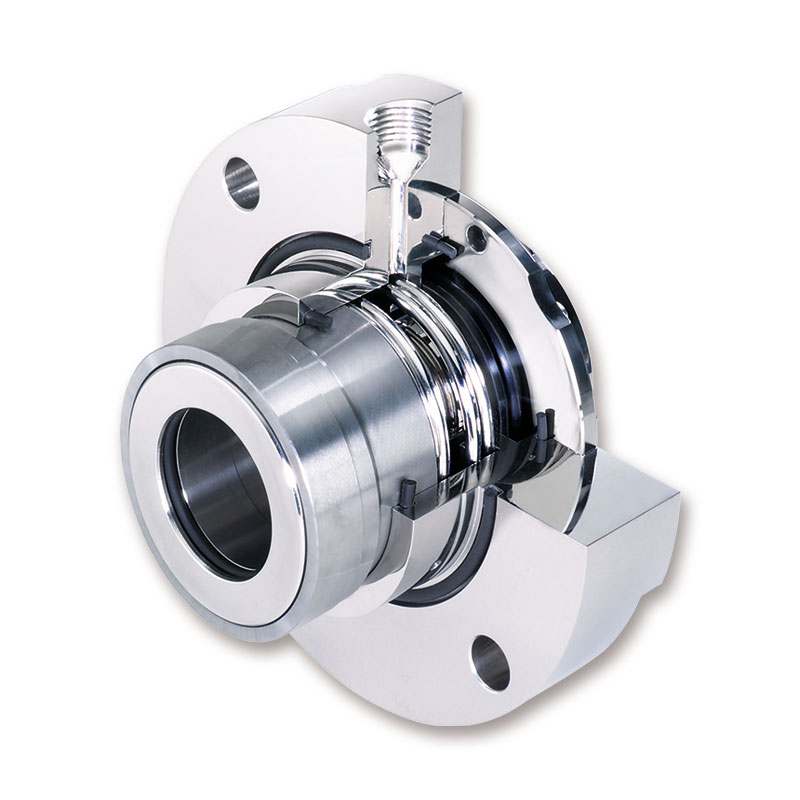
Heavy-duty Cartridge Slurry Seal
Available as a single or double seal, the Type 5860 is designed to operate in the harshest abrasive slurry environments...

Type 4610 O-Ring Pusher Seal
Compact, General-duty, Single Cartridge O-ring Seal
The Type 4610 single cartridge seal, available off-the-shelf the world over...

Type SB1A
Single, Heavy-duty Cartridge Seals
The Safeseal Type SB1A is a single-cartridge seal for use with clean fluids and lubricants. It is versatile, easy to install and maintain...

Type FFET O-Ring Pusher Seal
Single Cartridge O-ring Seal
Designed to Reduce Installation Time and Errors. The compactness of the FFET cartridge seal ensures that it will fit all ANSI and DIN stuffing boxes and offers an ideal upgrade from packing...

Type 5840
Cost-effective Cartridge Slurry Seal
Our Type 5840 single-cartridge seal encompasses many of the advantages associated with heavy-duty seal design...

Type CK-725 W-D Vessel and Mixer Seal
Mixer and Agitator Cartridge Seal to Vessel Seal Standard DIN 28138 for Steel Chemical Reaction Vessels — No Bearing Integrated
The Type CK 725 is a...

Diamond Seal Face Technology
John Crane Diamond® Unique Characteristics Extend Mechanical Seal Life
Derived from nature’s hardest substance…

Upstream pumping
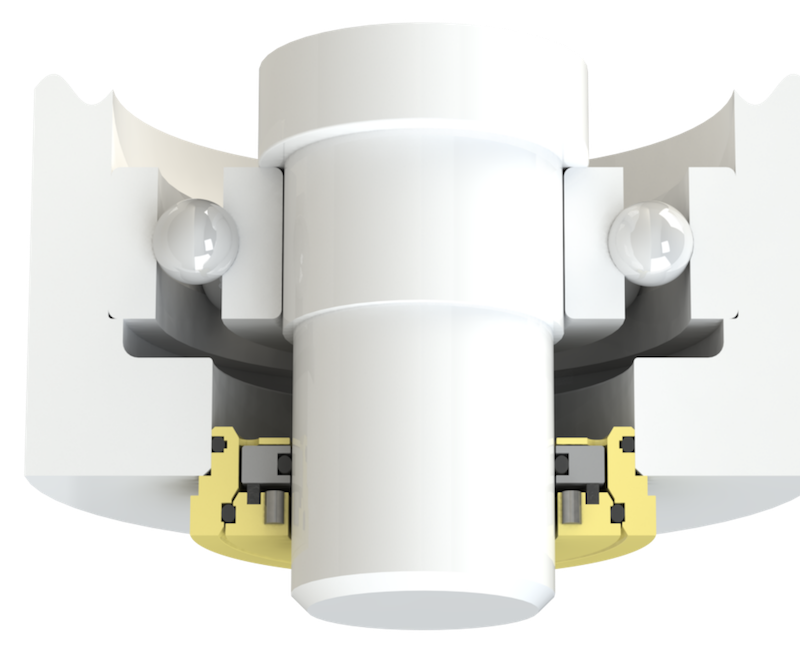
John Crane’s unique, engineered, non-contacting
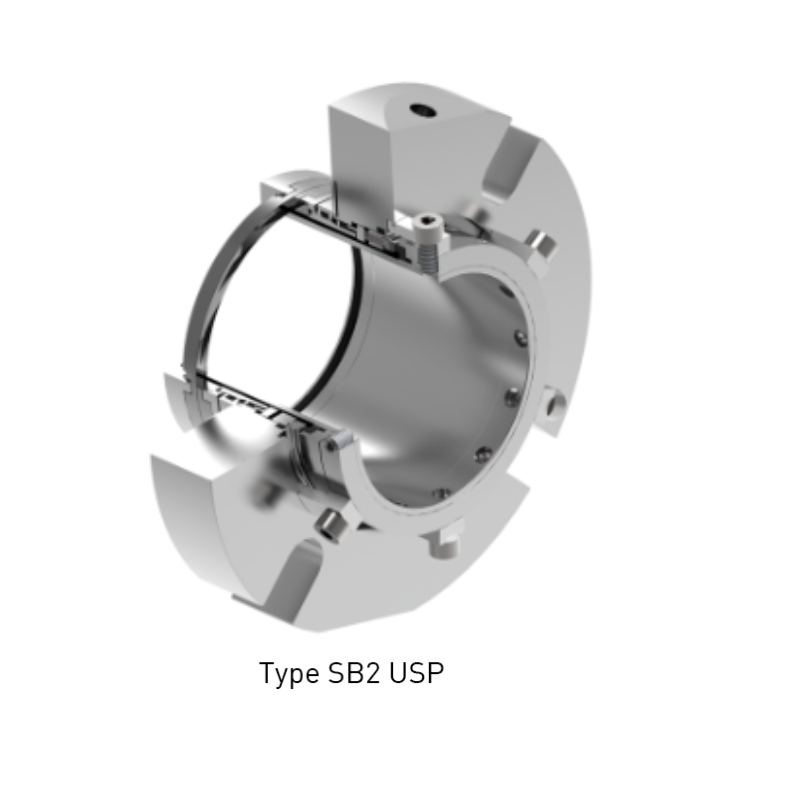
USP seal face technology borrows from gas seal designs to deliver a breakthrough in liquid sealing technology...

John Crane Mechanical Packing
Mechanical Packing Set
John Crane Packings are designed, engineered and constructed for specific services and applications...

1332/1335
General-service Braided Synthetic Packings
John Crane styles 1332 and 1335 are cost-effective general-service packings constructed of the highest-quality synthetic fibers and lubricants...

Abrasive Service Packing 1345–1349
Abrasive Service Polyimide Packings
John Crane styles 1345 and 1349 are constructed of high tensile strength abrasion resistant fibres...

K1730/K1761/K1771 Aramid Fiber Packing
Abrasive Service Aramid and Meta-aramid Packings
John Crane styles K1730, K1761 and K1771 are constructed of high-tensile strength...

CPR Bushing
Bushing
The CPR bushing is designed to reduce or restrict process media from entering the stuffing box or seal chamber and, in turn, extending the packing or mechanical seal life...

A Series
Wrap-fit Urethane Element Coupling
John Crane’s Powerstream® A Series coupling provides a solution to one of the most persistent and troublesome problems facing...

Metastream L Series Coupling Solutions
General-purpose All-metal Membrane Coupling
John Crane’s Metastream® L Series range of membrane (disc) couplings...

TSKL/TLKL Couplings
T Series Close Coupled Radially Split Coupling for Medium to High Torque Applications
John Crane’s Metastream® TSKL/TLKL Series of close-coupled membrane (disc) couplings...

TDK/TSK/TLK Disc Couplings
T Series Stainless Steel Discs in Pre-assembled Cartridge for Medium to High Torque Applications (Metric)
John Crane’s Metastream TDK/TSK/TLK Series are metallic membrane (disc) couplings...

Magnum-D V8
The Magnum-D V8 bearing isolator is the result of our dedicated mission to increase bearing life. It utilizes magnetically controlled lapped flat sealing faces in collaboration with ports on the atmospheric side for contaminant expulsion...

Magnum-P V7
The Magnum-P V7 bearing isolator is the result of our dedicated mission to increase bearing life...

Magnum-P V6s Bearing Isolator
The Magnum-P V6S bearing isolator is the result of our dedicated mission to increase bearing life. It utilizes magnetically controlled lapped flat sealing faces in collaboration with expulsion ports...

SafeJet Seal Water Filter System
Compact in-line seal water filter
SafeJet is an automatic seal water filter. Its operation is based on “flow-through” filter technology...

Seebach Inline Filters
John Crane’s Seebach® In-line filters are filter systems which are installed directly in the fluid line. Filter candles and filter cartridges are primarily used as filter elements...

High Capacity Filters
John Crane’s Seebach® highcapacity filters have been optimised through high surfaces and large inlet and outlet diameters for high flow rates (between 500-6000 l/min). We distinguish between single...
Solutions for every step of the mining process
Extraction
Technologies designed to protect equipment used in integrated systems for crushing, separating and transporting minerals for processing in demanding mining environments.
Milling / grinding
Solutions optimised to handle the suspended solids, coarse slurries and chemicals used to reduce materials into fine particles.
Separation
Products engineered to perform reliably when exposed to harsh chemicals and water common in mineral separation processes.
Refining
Our products help manage the arduous slurries, minerals and abrasives that characterize this stage of the mining and mineral processing industry.
Dewatering
Products recommended for moving large volumes of water.

John Crane Performance Plus™
John Crane Performance Plus™ is our modular service framework, supported by the largest mechanical seal service network, with over 200 manufacturing, sales and service centres globally. That means we are where you need us, when you need us – empowering people, plant and performance.
Further reading for the mining industry


Common questions
Why are mechanical seals important for mining equipment?
Mechanical seals play a critical role in mining equipment by helping control leakage, reduce water and energy consumption and extend equipment lifespan. John Crane’s mechanical seals for mining applications are designed for heavy-duty operation, helping mine operators reduce maintenance requirements and improve pump reliability in demanding conditions.
What are the best sealing solutions for the mining and mineral processing industry?
The best sealing solutions for the mining and mineral processing industry are designed to perform reliably in harsh environments involving abrasive slurries, chemicals and high water usage. John Crane offers mechanical seals and solutions engineered to help improve reliability, reduce leakage and support long-term operational performance.
How does John Crane support sealing reliability in mining operations?
John Crane supports sealing reliability in mining operations through a combination of engineered mining seals, advanced seal face technologies and global service expertise. Backed by Performance Plus, John Crane works closely with mining operators to assess sealing performance, address root causes of failure and improve overall equipment reliability.
What are John Crane’s solutions for packing?
Packing is often preferred by pump OEMs and mine operators. Upgrading to mechanical seals for mining applications can help address the economic and environmental issues mine operators face.
What are John Crane’s advanced sealing solutions?
Designed for harsh mining environments, the advanced materials and robust components of mechanical seals are constructed to help lower maintenance costs, improve pump mean time between repair, and reduce water and energy consumption. These benefits can be enhanced through the addition of seal face technologies such as Upstream Pumping or John Crane Diamond®, which are designed to improve performance in abrasive and chemically aggressive mining conditions.