
MECHANICAL SEALS, SEAL SYSTEMS AND FILTRATION FOR THE PHARMACEUTICAL INDUSTRY
Pharmaceutical

OVERVIEW
Product purity. Process reliability.
Pharmaceutical manufacturers face increasing demands to maintain product quality, improve efficiency and meet strict regulatory requirements.
Pharmaceutical operations must balance strict regulatory compliance with reliable performance. In batch manufacturing, changing temperatures, fluctuating pressures and varying fluid properties place rotating equipment under continuous stress, while demanding clean-in-place (CIP) and sterilise-in-place (SIP) routines add further strain, increasing the risk of downtime and process disruption.
John Crane’s mechanical sealing, filtration and support system technologies are manufactured from FDA-compliant materials and tested in ISO-certified facilities to support validation, product integrity and stable operation.
The result is reduced contamination risk and greater confidence in regulated environments.
John Crane solutions for the pharmaceutical industry
Mechanical seals, seal support systems and filtration technologies specifically designed to support hygienic processing, reduce contamination risk and improve equipment reliability in demanding operating conditions.
Vessel, mixer and agitator seals
Hygienic mechanical seals designed for high purity applications in mixers, agitators, filter dryers, thin film evaporators and de-foaming units.
Type CK, Type 7800 and Type 5280 seal families are engineered for glass, steel and special alloy vessels. Balanced seal faces and high-performance materials support reliable operation, while non-contacting designs help minimise wear and reduce contamination risk. All designs meet FDA, ISO, DIN and ATEX requirements.
Our vessel, mixer and agitator seals for the pharmaceutical industry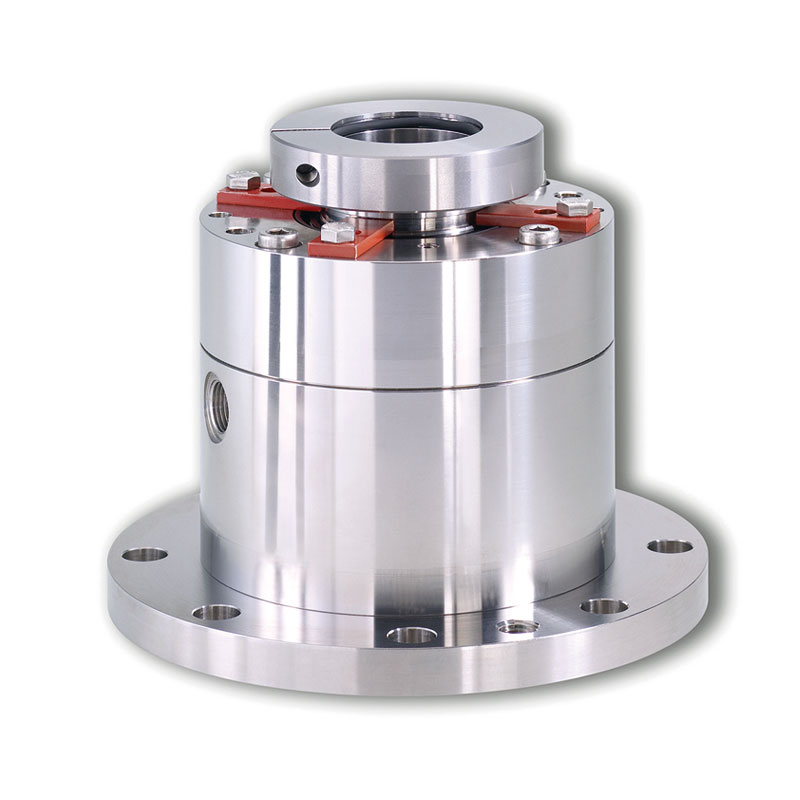
Cartridge seals
High-performance cartridge seals built for standard pumping applications where low emissions, reliability and ease of use are critical.
Manufactured from regulatory-compliant materials, these seals support safer operation, simplified installation and plant-wide standardisation.
The Type 5600 universal cartridge seal family covers a wide range of pharmaceutical duties, helping reduce downtime, improve efficiency and lower maintenance costs.
Single, dual, split, metal bellows and O-ring configurations are available.
Our cartridge seals for the pharmaceutical industry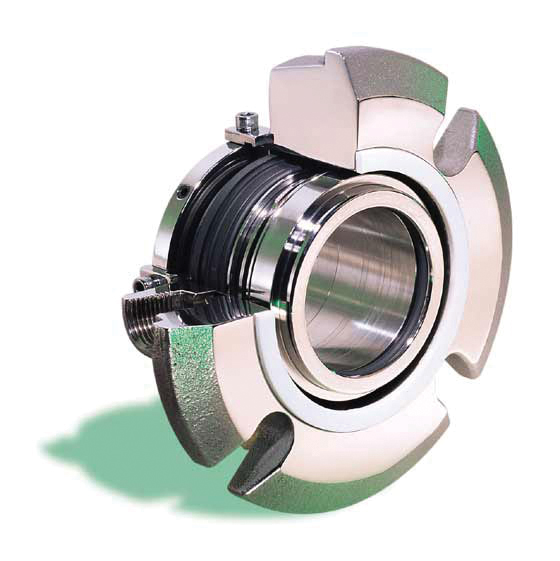
Pump seals
Advanced pump sealing solutions engineered for processes requiring the highest levels of contamination control.
Non-contacting pump gas seals use an inert gas lubricant to help protect product integrity and the external environment during demanding CIP and SIP cycles.
The Type 2800 delivers virtually zero process contamination for small bore rotating equipment, while the Type 2800E pressurised dual-cartridge design provides full containment even in the event of barrier gas pressure loss.
Our pump seals for the pharmaceutical industry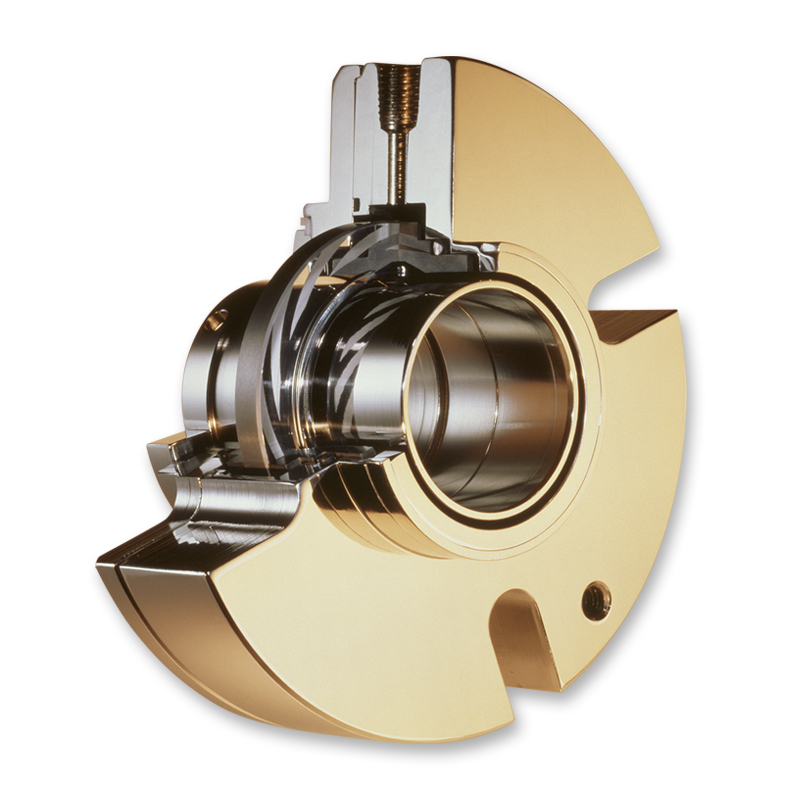
Metal bellows
Metal bellows seals for extreme temperatures, high pressures and aggressive chemical media where a cleanable seal profile is essential.
Formed and edge welded bellows options, including the Type GL1B, Type 515E, Type 515H, Type 604, Type 609, Type 680, Type 670 and Type 676, deliver reliable sealing across a wide range of services.
Our metal bellows seals for the pharmaceutical industry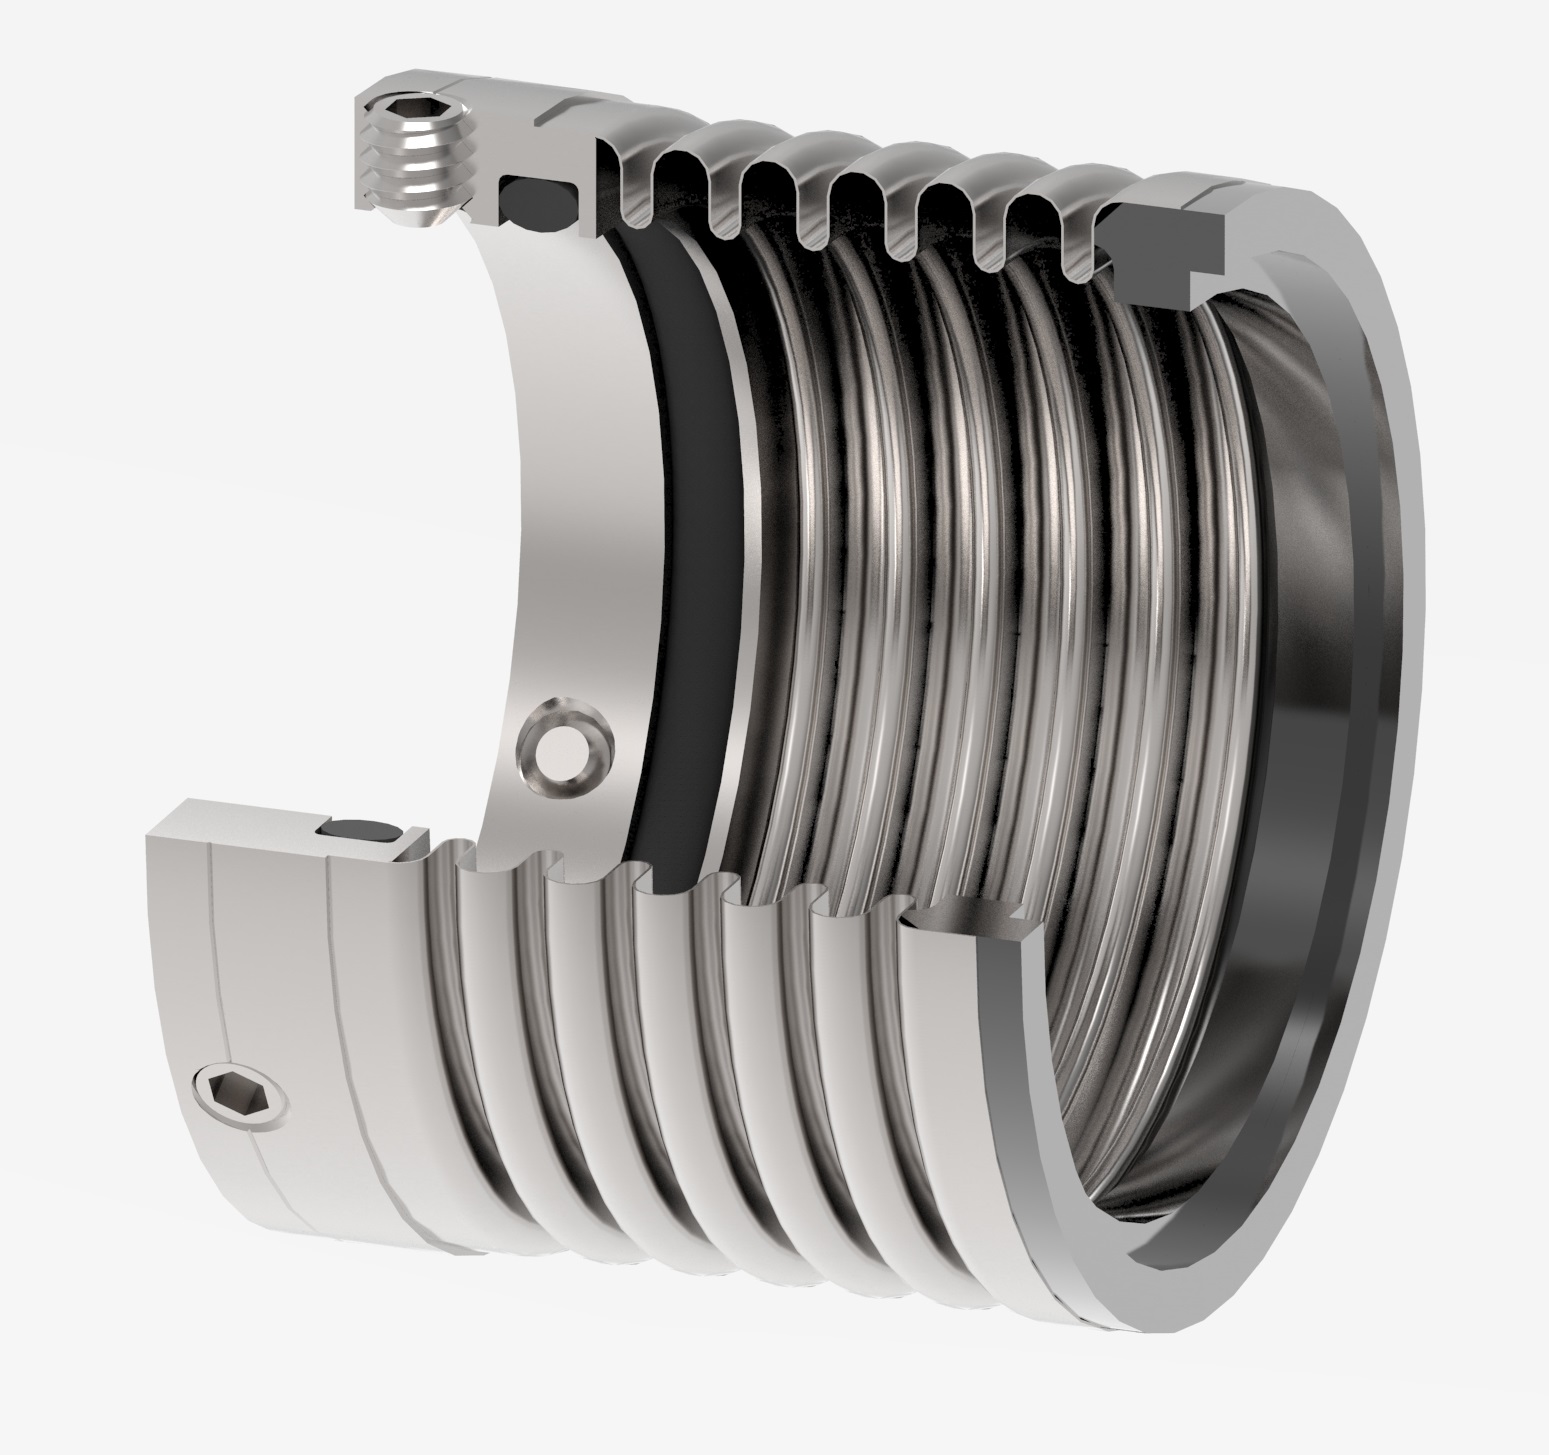
Seal support systems
Seal support systems engineered to maintain cleanliness, stability and reliability in critical pharmaceutical services.
Barrier fluid reservoirs, heat exchangers, gas supply panels and flush systems provide stable lubrication and cooling while reducing containment risk.
Integrated instrumentation enables monitoring of seal and system performance, and gas panels supply clean, inert lubrication to help prevent liquid contamination.
Systems can be supplied to meet ASME VIII, ASME B31.3, AD2000, ATEX, CE, PED and SELO requirements.
Our seal support systems for the pharmaceutical industry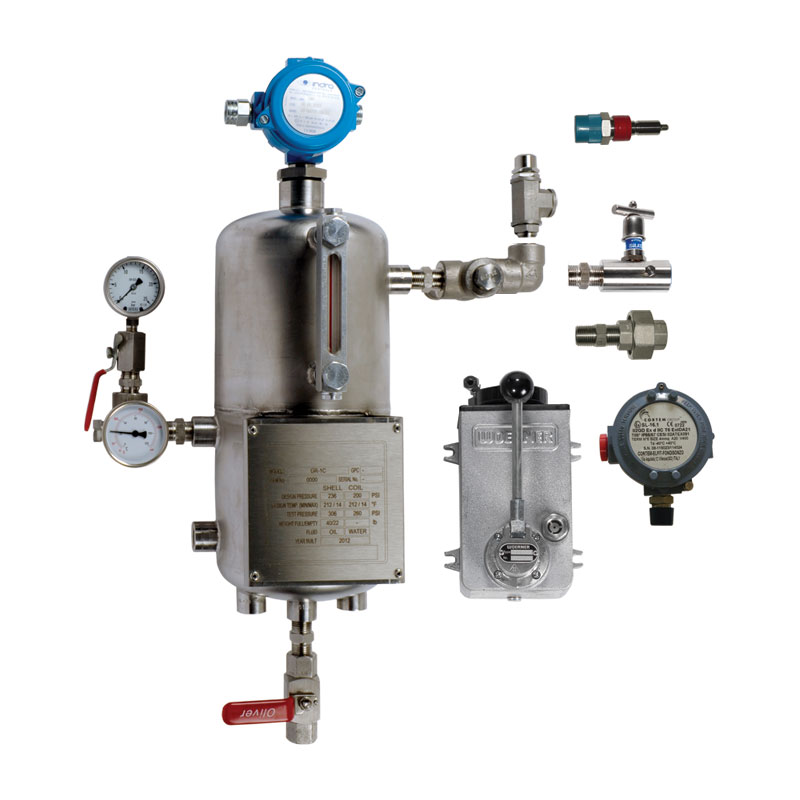
Filtration
Our filtration solutions support product purity, hygiene and process reliability throughout pharmaceutical operations.
John Crane Seebach® fully welded cylindrical CIP filter elements feature a star-shaped geometry and corrosion-resistant construction to support automated cleaning, including repeated CIP cycles.
Filter cones and baskets are designed to retain contaminants effectively while reducing the risk of bacterial growth. A wide range of filtration options is available, with fineness down to 0.2 microns for gases and 2 microns for liquids.
Our filtration solutions for the pharmaceutical industry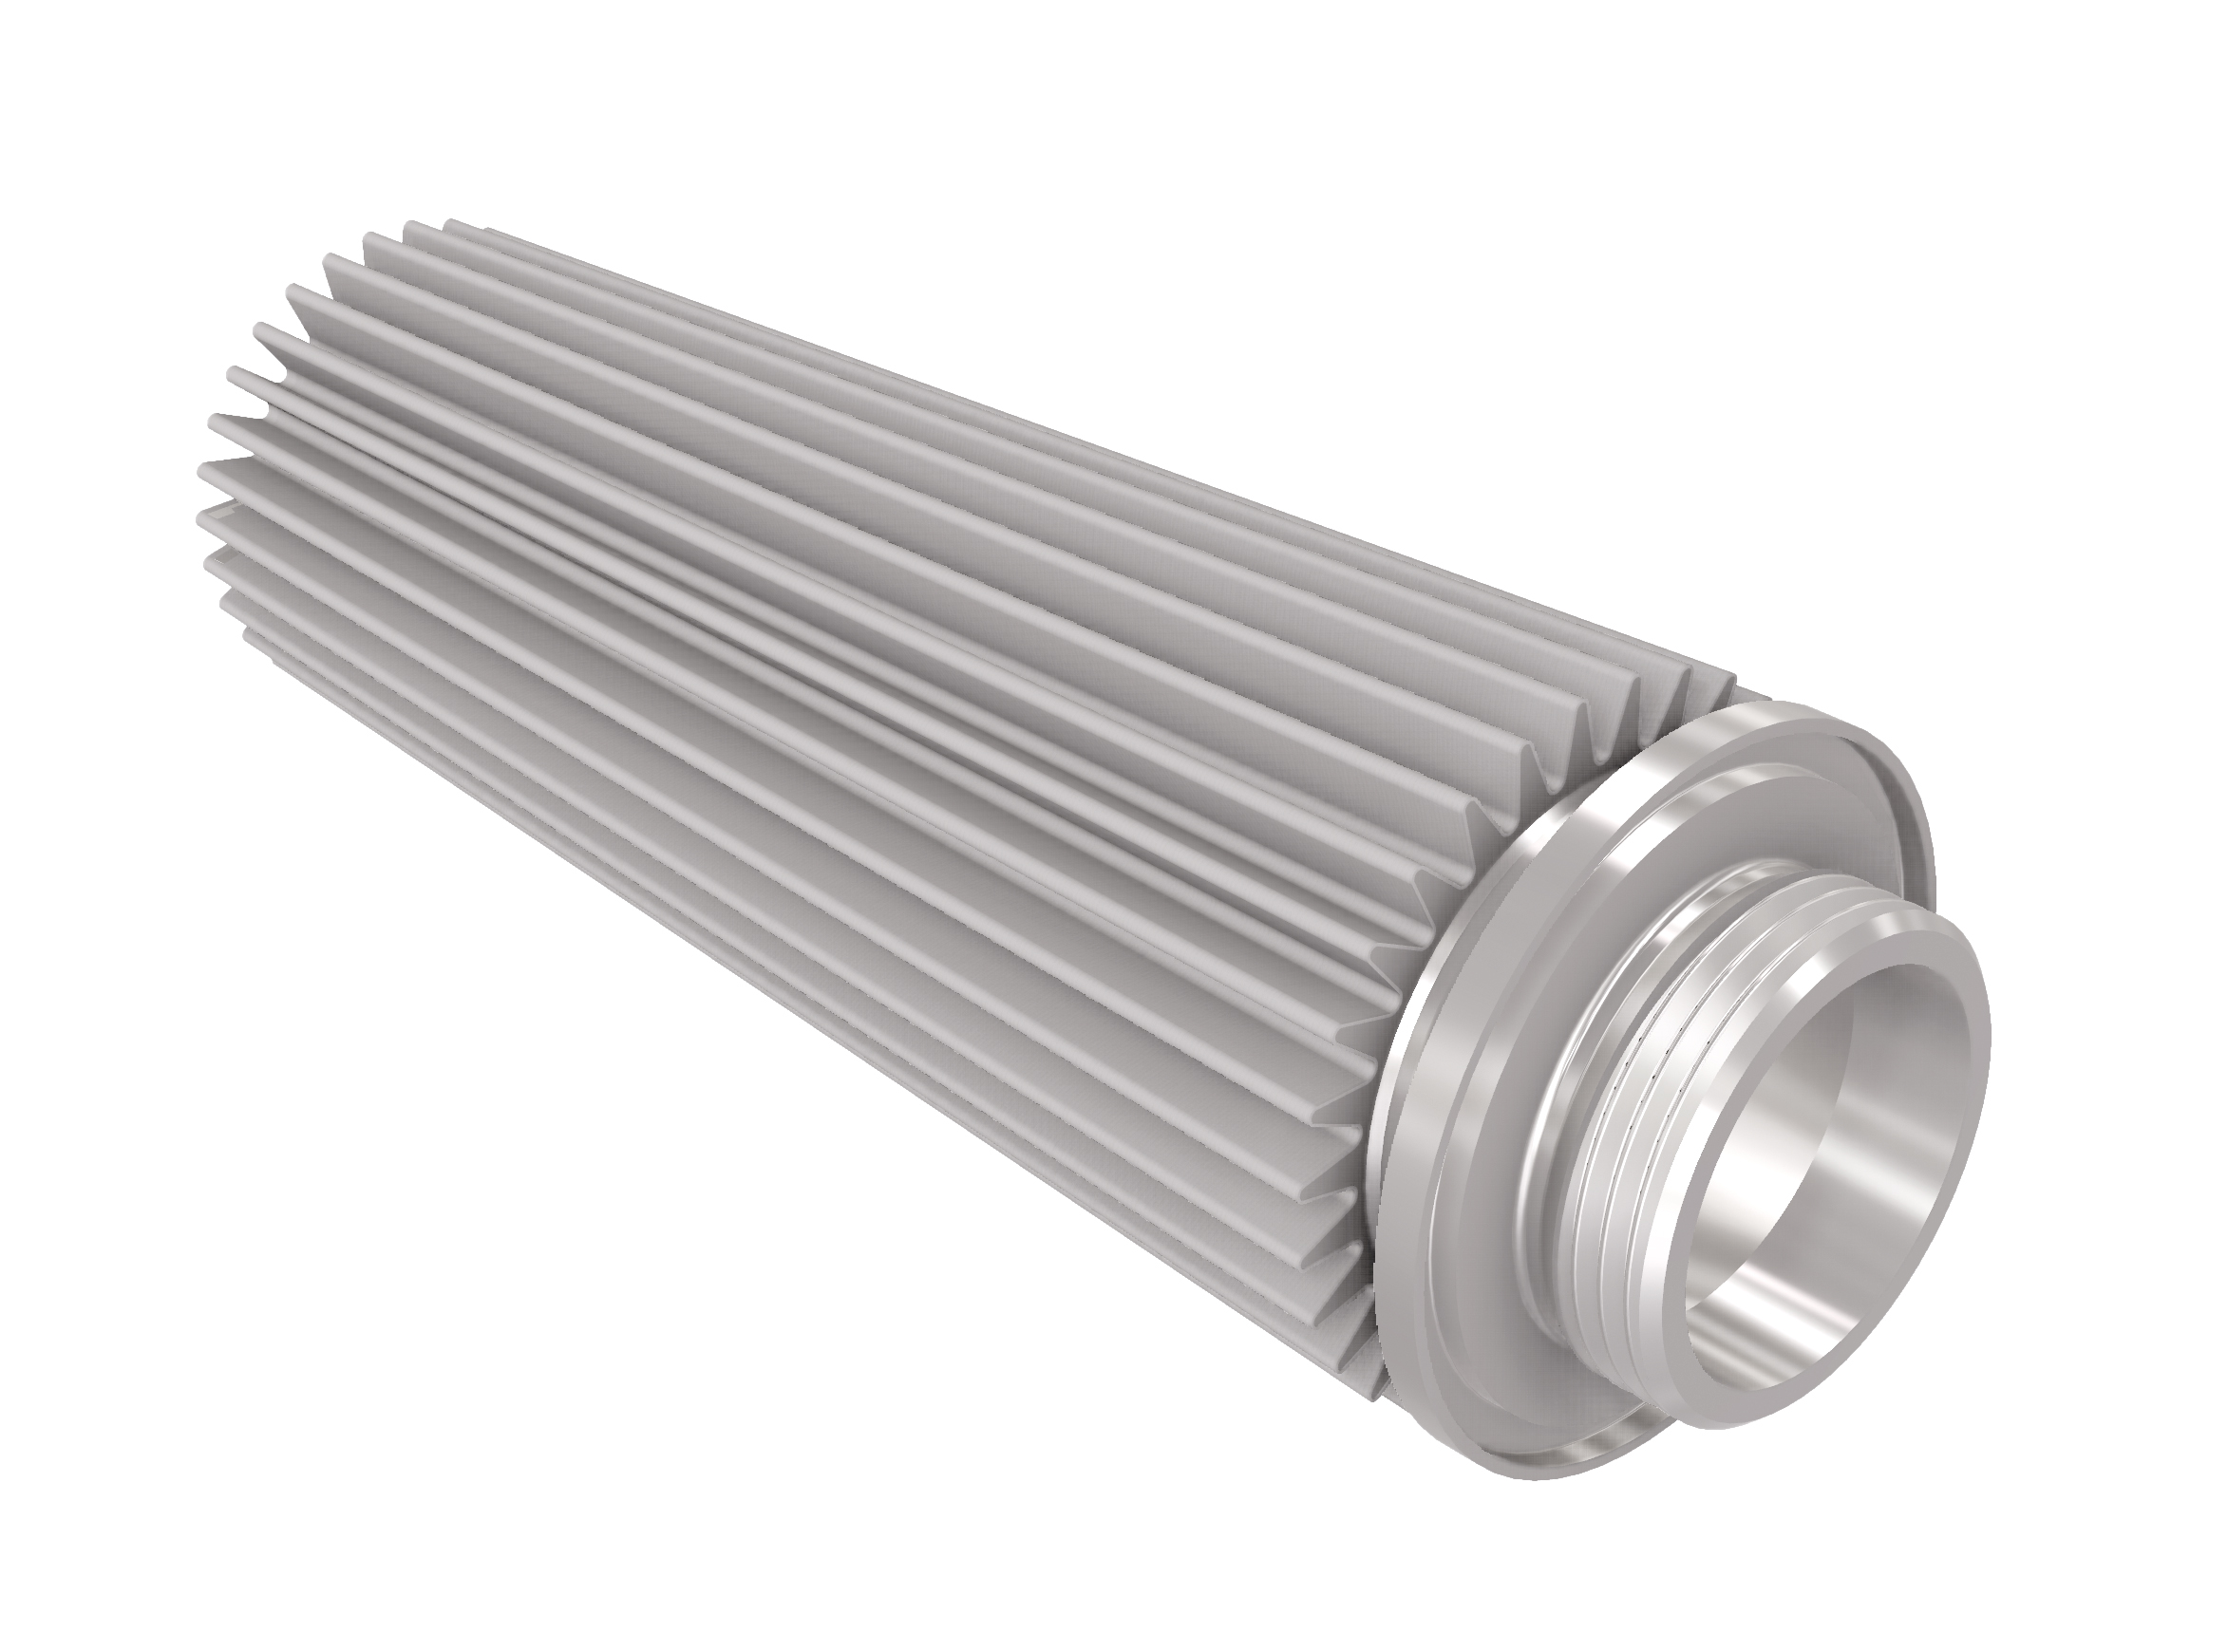

SUSTAINABILITY
Supporting your sustainability journey in pharmaceutical processing
Our sealing, filtration and support system technologies can help pharmaceutical manufacturers reduce leakage, extend equipment life and avoid unplanned maintenance. By supporting more reliable and efficient operation, they can also help reduce resource use and waste without compromising product integrity or regulatory compliance.
Our commitment to sustainabilityJohn Crane Performance Plus®
John Crane Performance Plus® is our modular service framework, supported by a global network of more than 200 manufacturing, sales and service centres. It combines maintenance support, reliability expertise and performance insight to help pharmaceutical manufacturers reduce downtime, manage equipment more effectively and improve long-term operational performance.
Common questions
Why is sealing critical in pharmaceutical manufacturing?
Sealing plays a key role in protecting product quality, maintaining hygienic conditions and supporting reliable equipment operation. Drawing on decades of applied engineering experience, John Crane helps manage leakage risks and reduce contamination potential to support processing across fluid-handling systems.
What should pharmaceutical companies look for in a sealing partner?
Pharmaceutical companies benefit from a sealing partner with strong engineering experience and global support capability. John Crane works closely with pharmaceutical processors to deliver application-specific sealing technologies backed by testing and service support throughout the equipment lifecycle.
How is sealing technology evolving in the pharmaceutical industry?
Sealing technologies continue to evolve to address increasing demands for efficiency, reliability and contamination control. John Crane develops pharmaceutical sealing solutions through ongoing investment in materials, non-contacting designs and testing methods that support continuous processing environments.
Further reading for the pharmaceutical industry


Doubling up: How dual mechanical seals can protect sensitive pharmaceutical processes (part 2)


